Water and wastewater treatment facilities require energy-efficient, reliable pumps for raw water intake, treatment processes, sludge handling, and effluent discharge. Pump performance directly affects treatment quality and operational costs.
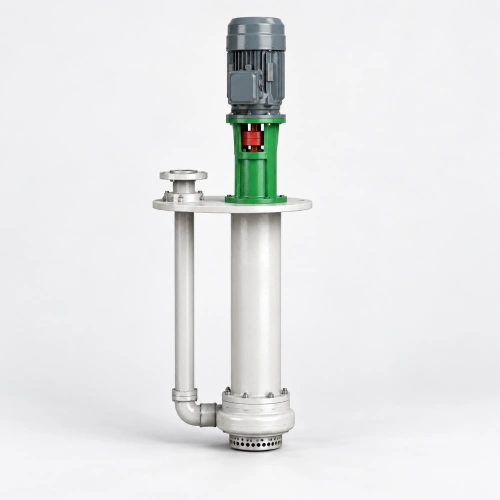
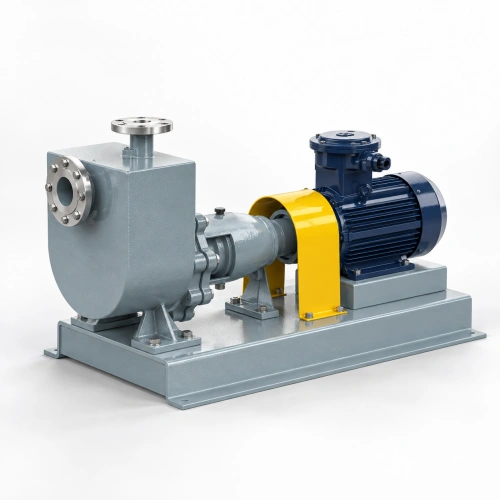
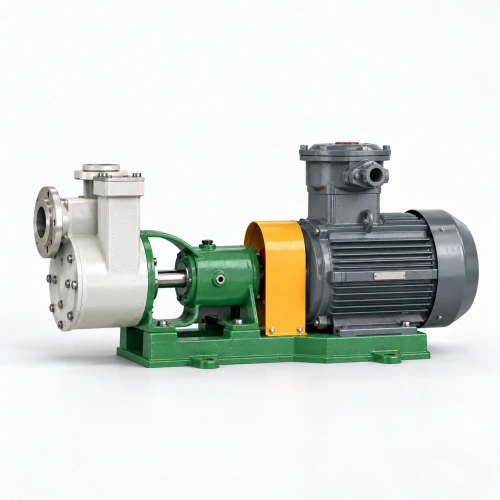
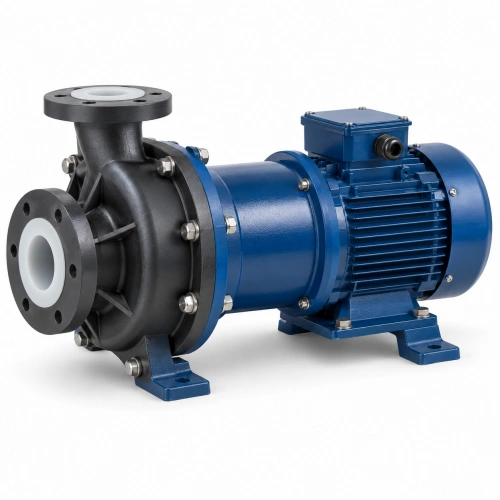
China Industrial Pump Network provides submersible sewage pumps, stainless steel self-priming pumps, vertical sump pumps, and split case pumps for water and wastewater applications. Our pumps feature non-clog impellers, corrosion-resistant materials, and high-efficiency hydraulic designs.
Water and wastewater pump selection balances efficiency, reliability, and solids handling capability. Consider fluid contamination level, submersible vs dry-pit installation, and energy costs over the pump lifecycle.
Classify as clean water, raw water, screened wastewater, unscreened sewage, or sludge. Solids size and concentration determine impeller passage and pump type. Use vortex impellers for stringy materials.
Submersible pumps for wet wells and sumps (no priming needed). Dry-pit horizontal pumps for easy maintenance. Vertical turbine for deep wells and raw water intake. Self-priming for portable service.
Water pumps often run continuously; prioritize high efficiency (IE3/IE4 motors, premium hydraulic designs). Calculate lifecycle cost: energy typically represents 80% of total cost over 10 years.
Cast iron for clean water; 316SS for brackish or seawater; duplex for high chloride; coated cast iron for mildly corrosive wastewater. Consider galvanic corrosion in mixed metal systems.
Mechanical seals for clean water; double mechanical seals for wastewater with abrasives; submersible seals with oil bath for sewage. Avoid packing in submersible service. Specify seal leak detection.
Include level controls (float, ultrasonic, pressure) for automatic operation. Variable frequency drives for variable flow systems. Consider remote monitoring for unmanned stations.
Carefully selected pump models that meet the specific requirements of the Water & Wastewater industry.
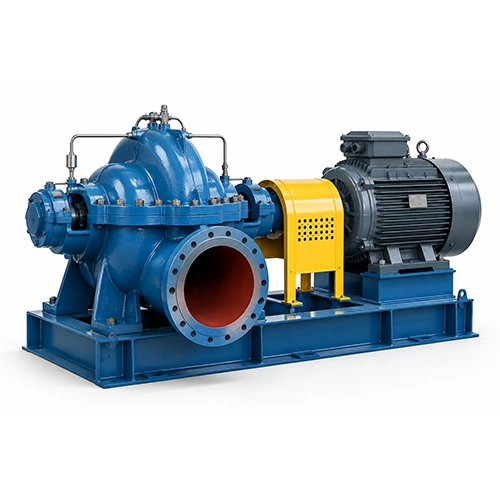
API 610 BB1 Double-Suction Split Case Process Pump
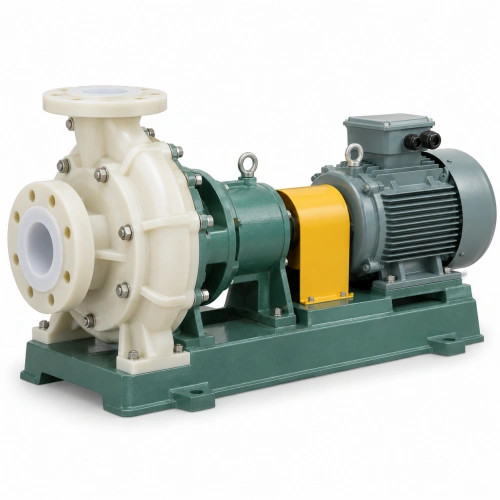
PTFE-Lined Centrifugal Pump for Corrosive Chemicals
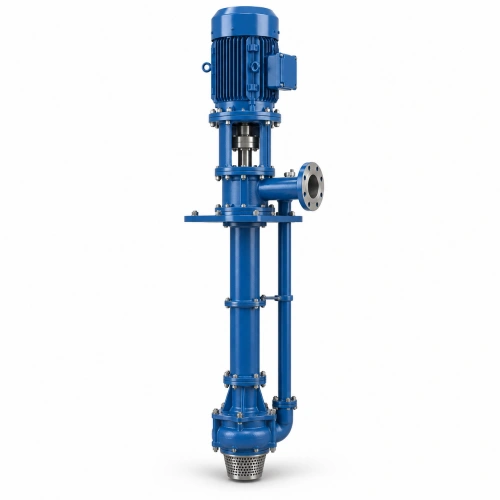
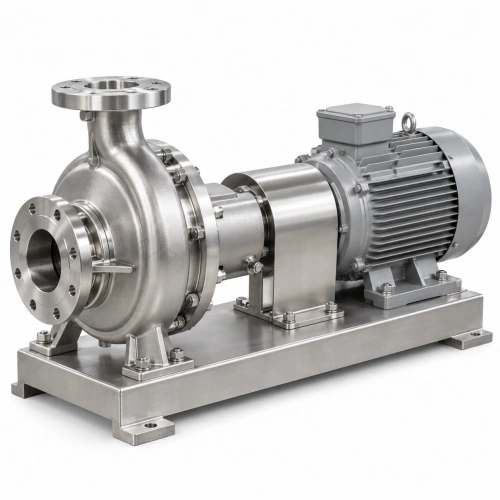
316L Stainless Steel Centrifugal Pump for Corrosive Chemicals
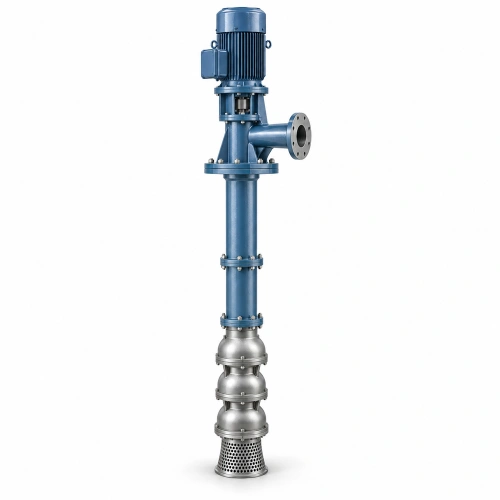
Sealless Leak-Free Centrifugal Pump for Hazardous Chemicals
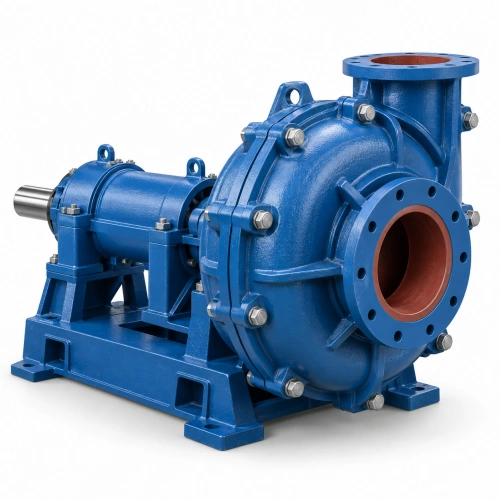
Heavy-Duty Centrifugal Slurry Pump for Mining & Mineral Processing
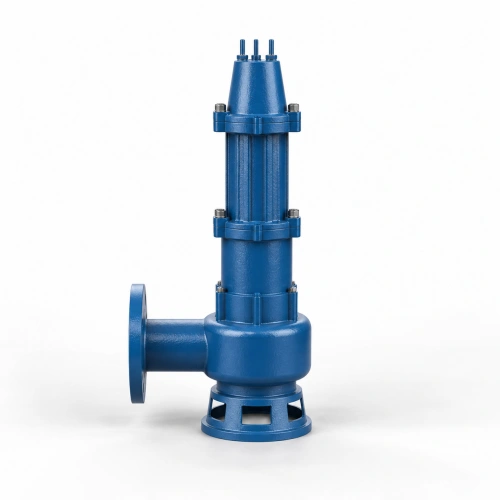
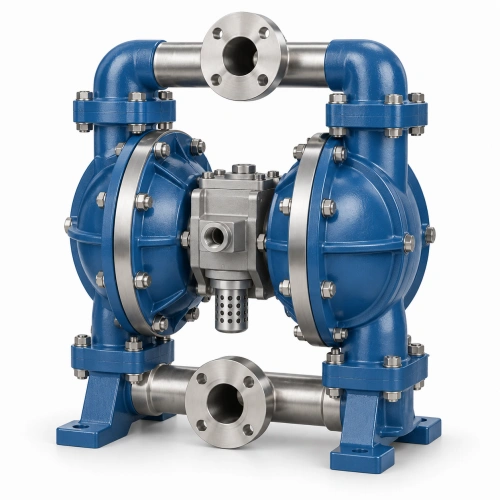
Air-Operated Double Diaphragm (AODD) Positive Displacement Pump
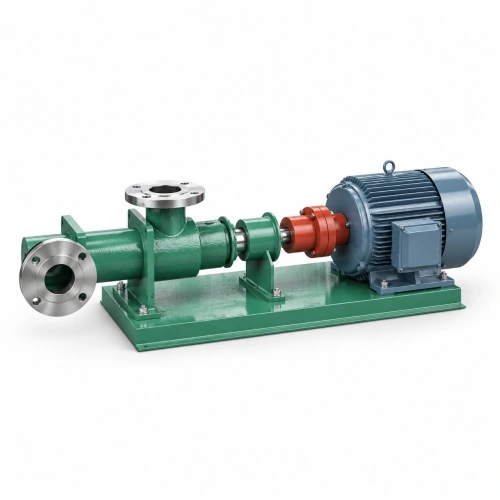
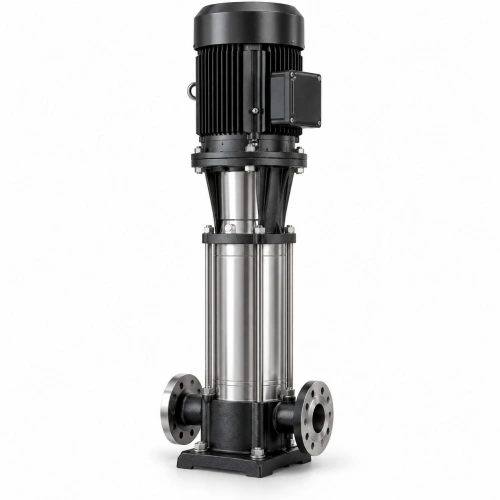
Compact Vertical Multi-Stage Pump for Water Supply and Pressure Boosting
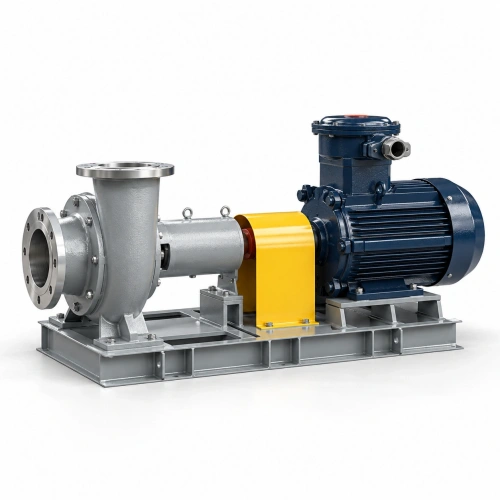
NFPA 20 Compliant Fire Protection Pump for Commercial & Industrial Applications
Our engineering team is ready to help you select the right pump for your application. Get a free quote today.