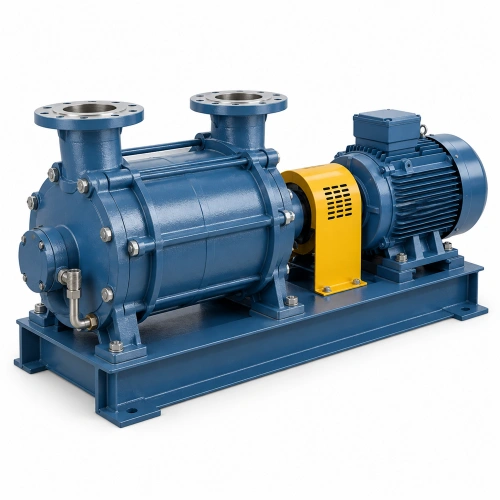
Liquid Ring Vacuum Pump
Oil-Free Vacuum Pump for Wet Gas Applications
Single-stage liquid ring vacuum pump for wet gas and vapor extraction. Handles moist, dusty, or condensable gases. Oil-free operation, reliable, low maintenance. Used in chemical, pharmaceutical, food, and pulp & paper industries.
Product Specifications
| Parameter | Range |
|---|---|
| Pumping Speed | 0.5 – 200 m³/min |
| Ultimate Vacuum | Down to -0.097 MPa (70 mmHg) |
| Liquid Ring | Water or compatible liquid |
| Temperature | Up to 80°C gas temp |
| Materials | Cast iron, 304SS, 316SS, bronze impeller |
| Seal | Mechanical seal or packing |
Product Description
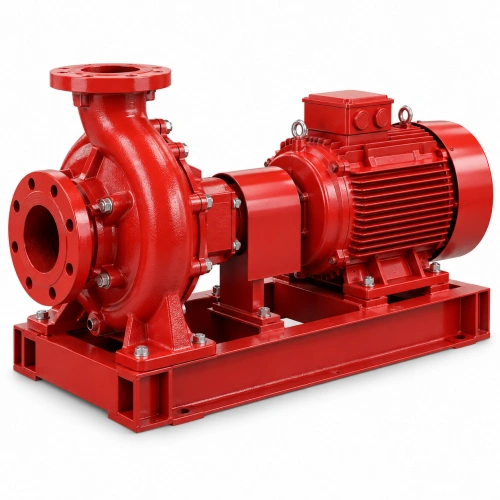
The Liquid Ring Vacuum Pump is a single-stage rotary positive displacement pump designed for wet gas and vapor extraction in industrial vacuum applications. Its liquid ring seal handles moist, dusty, or condensable gases without dry friction, providing reliable vacuum service with minimal maintenance. The pump operates at gas temperatures to 80°C, with cast iron or stainless steel construction and various seal liquid options. Ideal for filtration, degassing, vapor recovery, and process vacuum systems in chemical, food, and pharmaceutical industries.
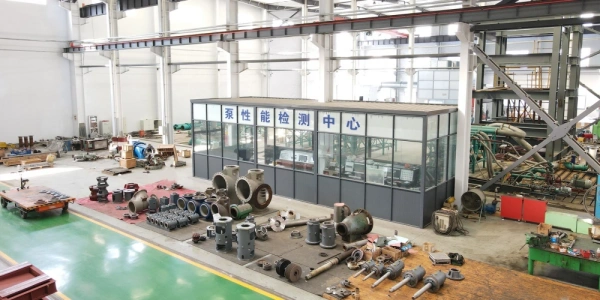
- Pumping speed and ultimate vacuum test
- Pressure test on casing
- Impeller balance inspection
- Mechanical seal leakage test
- Noise and vibration test
Applications
The Liquid Ring Vacuum Pump is used for gas and vapor extraction in various industries:
- Chemical processing and distillation
- Pharmaceutical manufacturing
- Food & beverage processing
- Pulp & paper industry
- Mining and mineral processing
Quality Assurance
Every vacuum pump is tested for performance and reliability:
Why Choose Our Special Industrial Pumps
Handles Wet and Dirty Gases
Liquid ring pumps tolerate moisture, dust, and condensable gases that would damage dry pumps.
Oil-Free Operation
No oil in the gas stream. Clean exhaust suitable for food and pharmaceutical applications.
Reliable, Low Maintenance
Few moving parts, simple design. Long service life with minimal maintenance.
Key Features
Frequently Asked Questions
What is a liquid ring vacuum pump used for?
How does a liquid ring vacuum pump work?
What liquid is used in a liquid ring pump?
What is the difference between liquid ring and dry vacuum pumps?
Selection Guide
✅ When to Choose This Pump
- Power plant cooling water and boiler feed
- Municipal water supply and distribution
- Very high flow circulation systems
- Multistage high-pressure applications
⚠️ When NOT to Choose
- Small batch chemical processing
- Corrosive acid handling
- Portable or mobile service
- Hygienic food applications
💡 Common Selection Mistakes
- Not calculating system curve properly
- Ignoring parallel pump operation effects
- Under-sizing suction piping
- Not considering water hammer effects
Still unsure? Use our Pump Selection Center → or talk to our engineers →
Interested in this product?
Contact our sales team for pricing, lead time, and technical support.
Send Inquiry Now